China Top Swiss Turning Services for Titanium Bone Screws
China has become a significant sourcing destination for precision medical components, including titanium bone screws. Swiss Turning Services For Titanium Bone Screws require more than fast cycle times. They demand controlled cutting, stable tooling, clean handling, and documented inspection. Titanium can generate heat quickly during machining. It may also react poorly to careless feeds, worn inserts, or inadequate chip evacuation.
Dr. Thomas J. Webster, a respected biomaterials researcher, offers a useful principle: “Material choice must serve both biological safety and mechanical performance.” That principle applies directly to titanium screw production. A capable Swiss-type machining partner should understand thread accuracy, head geometry, surface condition, and burr control. It should also verify critical dimensions with calibrated equipment. Small errors matter here. A damaged thread can affect insertion torque and surgical handling.
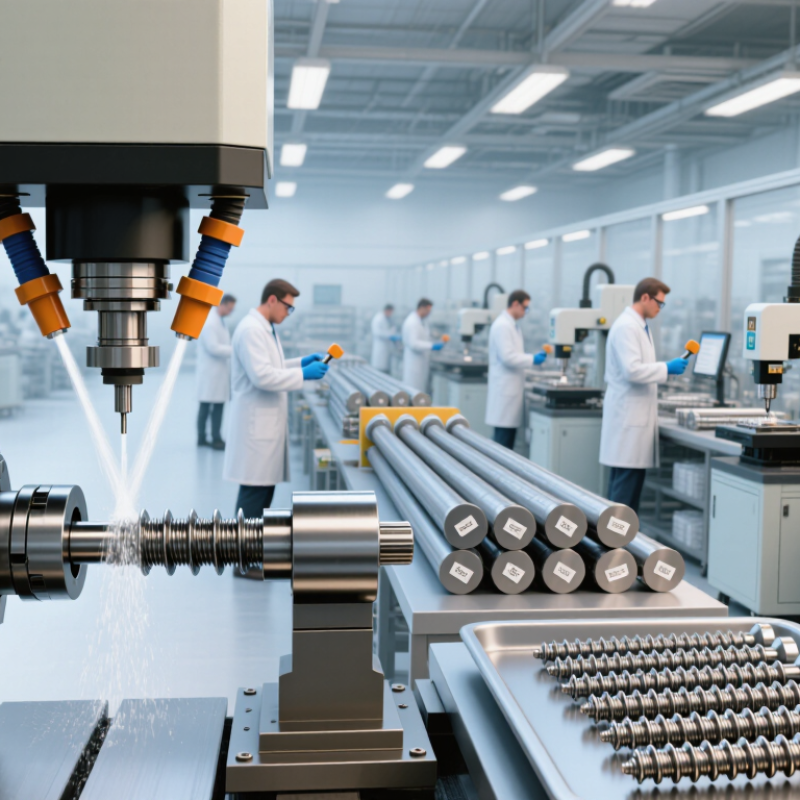
The strongest Chinese suppliers combine experienced machinists with process engineers and traceable quality systems. They may use high-pressure coolant, dedicated workholding, and in-process monitoring. Titanium bar stock should remain identifiable from receipt through final packaging. Cleanliness also deserves attention, especially when components enter controlled medical-device workflows.
Still, no supplier is perfect. A polished website cannot replace audit evidence, sample inspection, and direct technical discussion. Buyers should review material certificates, inspection reports, equipment capability, and corrective-action records. They should ask difficult questions early. That is where confidence begins.
Swiss Turning Services For Titanium Bone Screws should be evaluated through repeatability, transparency, and real manufacturing experience. Cost matters, but unstable quality costs more. The best partnership is measurable, careful, and willing to improve.
Titanium Bone Screws: Purpose, Design, and Clinical Applications
China Top Swiss Turning Services for Titanium Bone Screws
Titanium bone screws stabilize fractures, plates, spinal systems, and selected dental implants. Their purpose is mechanical support during bone healing. Titanium alloys offer high strength, low density, and strong corrosion resistance. Ti-6Al-4V remains widely used in orthopedic devices. ISO 5832-3 specifies requirements for this alloy’s chemical and mechanical performance. The MarketsandMarkets 2024 orthopedic implants report projects the sector to grow at roughly 5% annually through 2028. Demand is rising, but growth does not replace clinical judgment.
Design controls fixation quality. Cortical screws use finer threads and smaller pitch. Cancellous screws use deeper threads for softer bone. Cannulated designs guide placement over a wire. Self-tapping tips can reduce drilling steps, though they may increase heat or debris when technique is poor. Swiss turning can produce consistent threads, sharp transitions, and controlled head geometry in small titanium components. Yet dimensional accuracy alone is not enough. Surface finish, burr removal, cleaning, packaging, and traceability also affect safety. A 2023 FDA report on medical-device quality emphasizes documented process control and risk management across production stages.
Tips: Match thread geometry to bone density and anatomy. Verify torque limits with validated instruments. Inspect every lot for burrs, scratches, and thread damage. Clinical feedback should shape redesign. No screw is perfect; excessive stiffness may alter load transfer, while weak fixation can fail early. Surgeons and engineers must review both outcomes and unexpected complications.
Why Swiss Turning Suits Titanium Bone Screw Manufacturing
Swiss Turning Services for Titanium Bone Screws
Swiss turning suits titanium bone screw manufacturing because it controls small parts close to the cutting tool. This support reduces deflection during threading, drilling, and head formation. Titanium is strong, light, and difficult to machine consistently. It can generate heat quickly and react poorly to careless cutting conditions. A sliding-headstock machine helps maintain stability across long, narrow screw profiles. It also supports efficient production of miniature features.
Precision matters here.
Experienced machinists monitor tool wear, spindle speed, coolant flow, and chip evacuation throughout the run. Sharp, application-specific tools can reduce burrs around threads and drive recesses. Controlled feed rates help protect thread geometry and surface quality. In-process gauging can check critical diameters before a full batch is completed. Traceable inspection records support reliable manufacturing decisions and later review.
Swiss turning does not remove every risk. That assumption can fail. Titanium may still distort if clamping pressure or heat control is neglected. Tool changes, setup variation, and cleaning processes also deserve attention. A dependable process combines stable machining with calibrated gauges, documented inspections, and careful operator judgment. For bone screws, manufacturers should verify dimensional accuracy, surface condition, material records, and applicable quality requirements. Small details matter.
Material Selection and Precision Machining Requirements
Swiss turning for titanium bone screws demands disciplined material selection and precise machining control. Titanium alloys offer high strength, corrosion resistance, and good biocompatibility. However, they conduct heat poorly during cutting. Heat can remain near the tool edge and damage the surface.
Experienced machinists select certified bar stock with controlled chemistry and consistent grain structure. Each batch should have clear traceability. Important checks include diameter, straightness, hardness, and surface condition. Swiss machines support stable feeding and accurate production of threads, slots, and small diameters. Sharp tooling, suitable coatings, and controlled cutting speeds help reduce burrs and work hardening. Coolant delivery must reach the cutting zone directly.
Tips: Use generous chip clearance and inspect thread roots under magnification. Measure critical features after temperature stabilization. Record tool wear before it affects tolerance.
Precision is not only about machine capability. It also depends on setup quality, fixture stability, and inspection timing.
Coordinate measuring systems can verify diameter, pitch, concentricity, and runout. Visual inspection remains useful for scratches, burrs, and edge damage. A practical weakness is assuming one cutting recipe suits every titanium batch. It does not. Reviewing failed parts and adjusting parameters creates a more reliable process. Clean handling also matters because embedded particles may affect later finishing or clinical performance.
Quality Control Standards for Swiss-Turned Bone Screws
China’s Swiss turning services for titanium bone screws rely on disciplined quality control at every production stage. The process begins with certified titanium bar stock, commonly selected to meet applicable implant-grade material standards. Each batch receives identity checks, chemical verification, and traceable records before machining starts.
Swiss-type machines hold tight dimensions for threads, drive features, and screw diameters. Inspectors use calibrated optical systems, micrometers, and thread gauges to verify critical areas. Burrs matter. Even a tiny burr can affect insertion or tissue contact. Surface roughness, concentricity, and thread form also require documented inspection. Sampling alone may miss an unusual defect, so critical features often receive expanded checks.
Cleanliness control follows machining. Components should undergo validated washing, drying, and controlled handling before packaging. Visual inspection under magnification can reveal chips, discoloration, or trapped coolant. Mechanical testing may assess torsional strength, fatigue resistance, and insertion performance against defined specifications. Quality systems should align with relevant medical-device requirements, including risk management, process validation, and full lot traceability.
A reliable supplier keeps inspection reports, machine records, nonconformance logs, and corrective actions available for review. This supports experience-based decisions, not attractive claims. Still, no inspection plan is perfect. Tool wear can develop between scheduled checks. Environmental control can also be overlooked. Regular audits, operator training, and trend analysis help expose these weak points before they affect finished screws.
China Top Swiss Turning Services for Titanium Bone Screws
Quality Control Standards for Swiss-Turned Bone Screws
This reference chart presents commonly specified inspection targets for precision titanium bone screws, including dimensional accuracy, thread geometry, concentricity, surface finish, and material traceability. Actual acceptance limits are controlled by the approved engineering drawing, inspection plan, and applicable medical-device requirements such as ASTM F136, ISO 5832-3, and ISO 13485.